product
Industrial Water Treatment Equipment
- TOP
- Browse by Product
- Industrial Water Treatment Equipment
- Sand Separator (Desanding Cyclone System)
Sand control for groundwater,
industrial water, and other water sources
Sand Separator (Desanding Cyclone System)
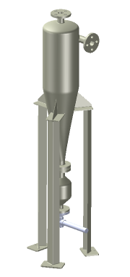
The Sand Separator efficiently removes sand and fine solids from groundwater, river water, and industrial water using a cyclone (centrifugal separation) method. It helps reduce sand inflow into pumps, membrane treatment systems, and filtration systems, helping prevent equipment wear and clogging. Made of highly durable stainless steel, it supports stable long-term operation.
Main Applications
- Sand removal from groundwater, river water, and industrial water
- Pretreatment for cooling water and boiler feedwater
- Protective pretreatment for membrane treatment systems (RO/UF) and pumps
Main Industries and Facilities
The Sand Separator can be used across a wide range of industries and facilities that need to control sand in raw water.
- Electronics
- Chemicals, materials, and machinery
- Pharmaceuticals, cosmetics, and medical devices
- Hospitals and welfare facilities
- Hotels and commercial facilities
- Food manufacturing
Advantages and Benefits
Protecting Downstream Equipment
Installed upstream of pumps, piping, boilers, cooling towers, filtration systems, and other equipment, the Sand Separator helps reduce the inflow of sand and solids to help prevent wear and clogging.
Expected Benefits
- Reduced replacement and repair costs through longer equipment service life
- Reduced frequency of backwashing and cleaning
Space-saving Compared with Sand Settling Tanks
With a significantly more compact structure than conventional sand settling basin or sand settling tank systems, the Sand Separator is designed for easy installation at sites with limited space and during upgrades of existing equipment.
Expected Benefits
- Reduced installation space
- Reduced scale of civil engineering work
Reduced Maintenance Workload
The Sand Separator removes sand using the cyclone effect (centrifugal force) generated inside the unit by the velocity of the raw water. Its simple structure requires no internal power source, filter media, or chemicals, helping reduce maintenance workload and enabling stable continuous operation.
Expected Benefits
- Reduced filter media and chemical costs
- Reduced operation management workload
Durable Stainless-steel Construction
The main unit is made of stainless steel, supporting stable operation over the long term. Compared with commonly used carbon steel construction, stainless steel offers stronger resistance to corrosion and aging, and can accommodate a variety of raw water conditions, including well water, river water, and cooling water.
Expected Benefits
- Longer equipment service life
- Prevention of water quality deterioration caused by corrosion and rust
How the Sand Separator Works
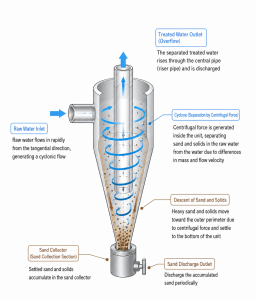
Raw water enters the unit tangentially, generating a swirling flow (cyclone) inside the separator. Sand and solids in the raw water are pushed toward the inner wall by centrifugal force and move downward by their own weight. Treated water rises through the center of the unit and is discharged from the outlet at the top.
Sand and solids accumulate at the bottom of the unit and are discharged through the sand discharge valve as needed. Manual and automatic sand discharge valves are available depending on operating conditions.
Integrated Industrial Water Treatment System Solutions
In addition to the Sand Separator, AMCON provides optimal system configurations based on raw water quality and application.
- Iron and Manganese Removal Filter: Removal of iron and manganese in well water and groundwater
- Rapid Sand Filter: Removal of turbidity and fine particles
- Activated Carbon Filter: Adsorption of residual chlorine, organic matter, and odor components
- Ion Exchange Water Softener: Removal of hardness components
AMCON provides integrated support covering water quality analysis, equipment selection, filter media selection, new equipment installation, removal and replacement of existing equipment, and After-Sales Support including filter media replacement.
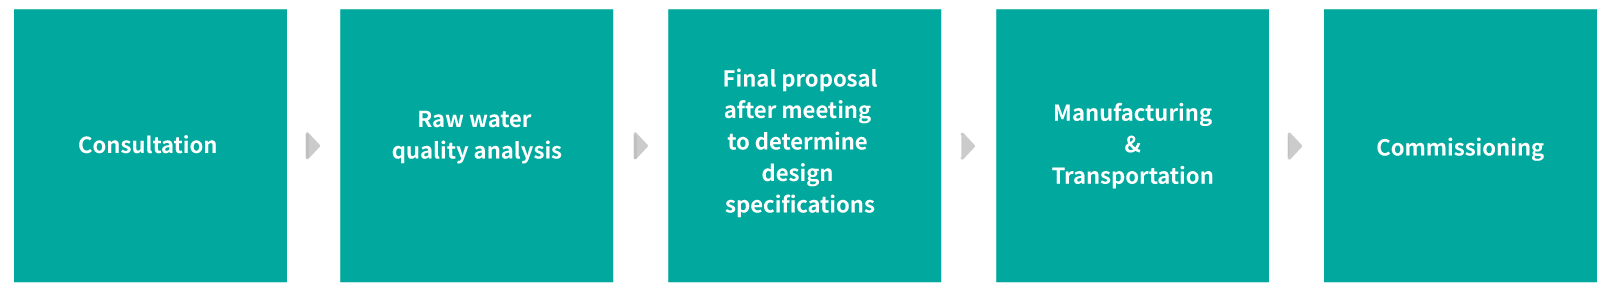
Feel free to contact us for an initial consultation. After reviewing current water quality challenges, application, requirements, installation site, and other conditions, AMCON proposes specifications suited to the customer. In raw water quality analysis, the components present and target substances to be removed are confirmed, and AMCON determines whether the Sand Separator can be introduced as a standalone unit or whether it should be combined with other Industrial Water Treatment equipment. Once specifications and auxiliary equipment are determined, the unit is manufactured, delivered, installed, commissioned, and handed over.